Mechanical Engineering
Assembly System with 60 kN Press for Aluminium Components
Realization of an assembly system for pressing sleeves and threaded bolts into aluminium components, for the manual assembly of special elements, and for subsequent measurement.
Challenge
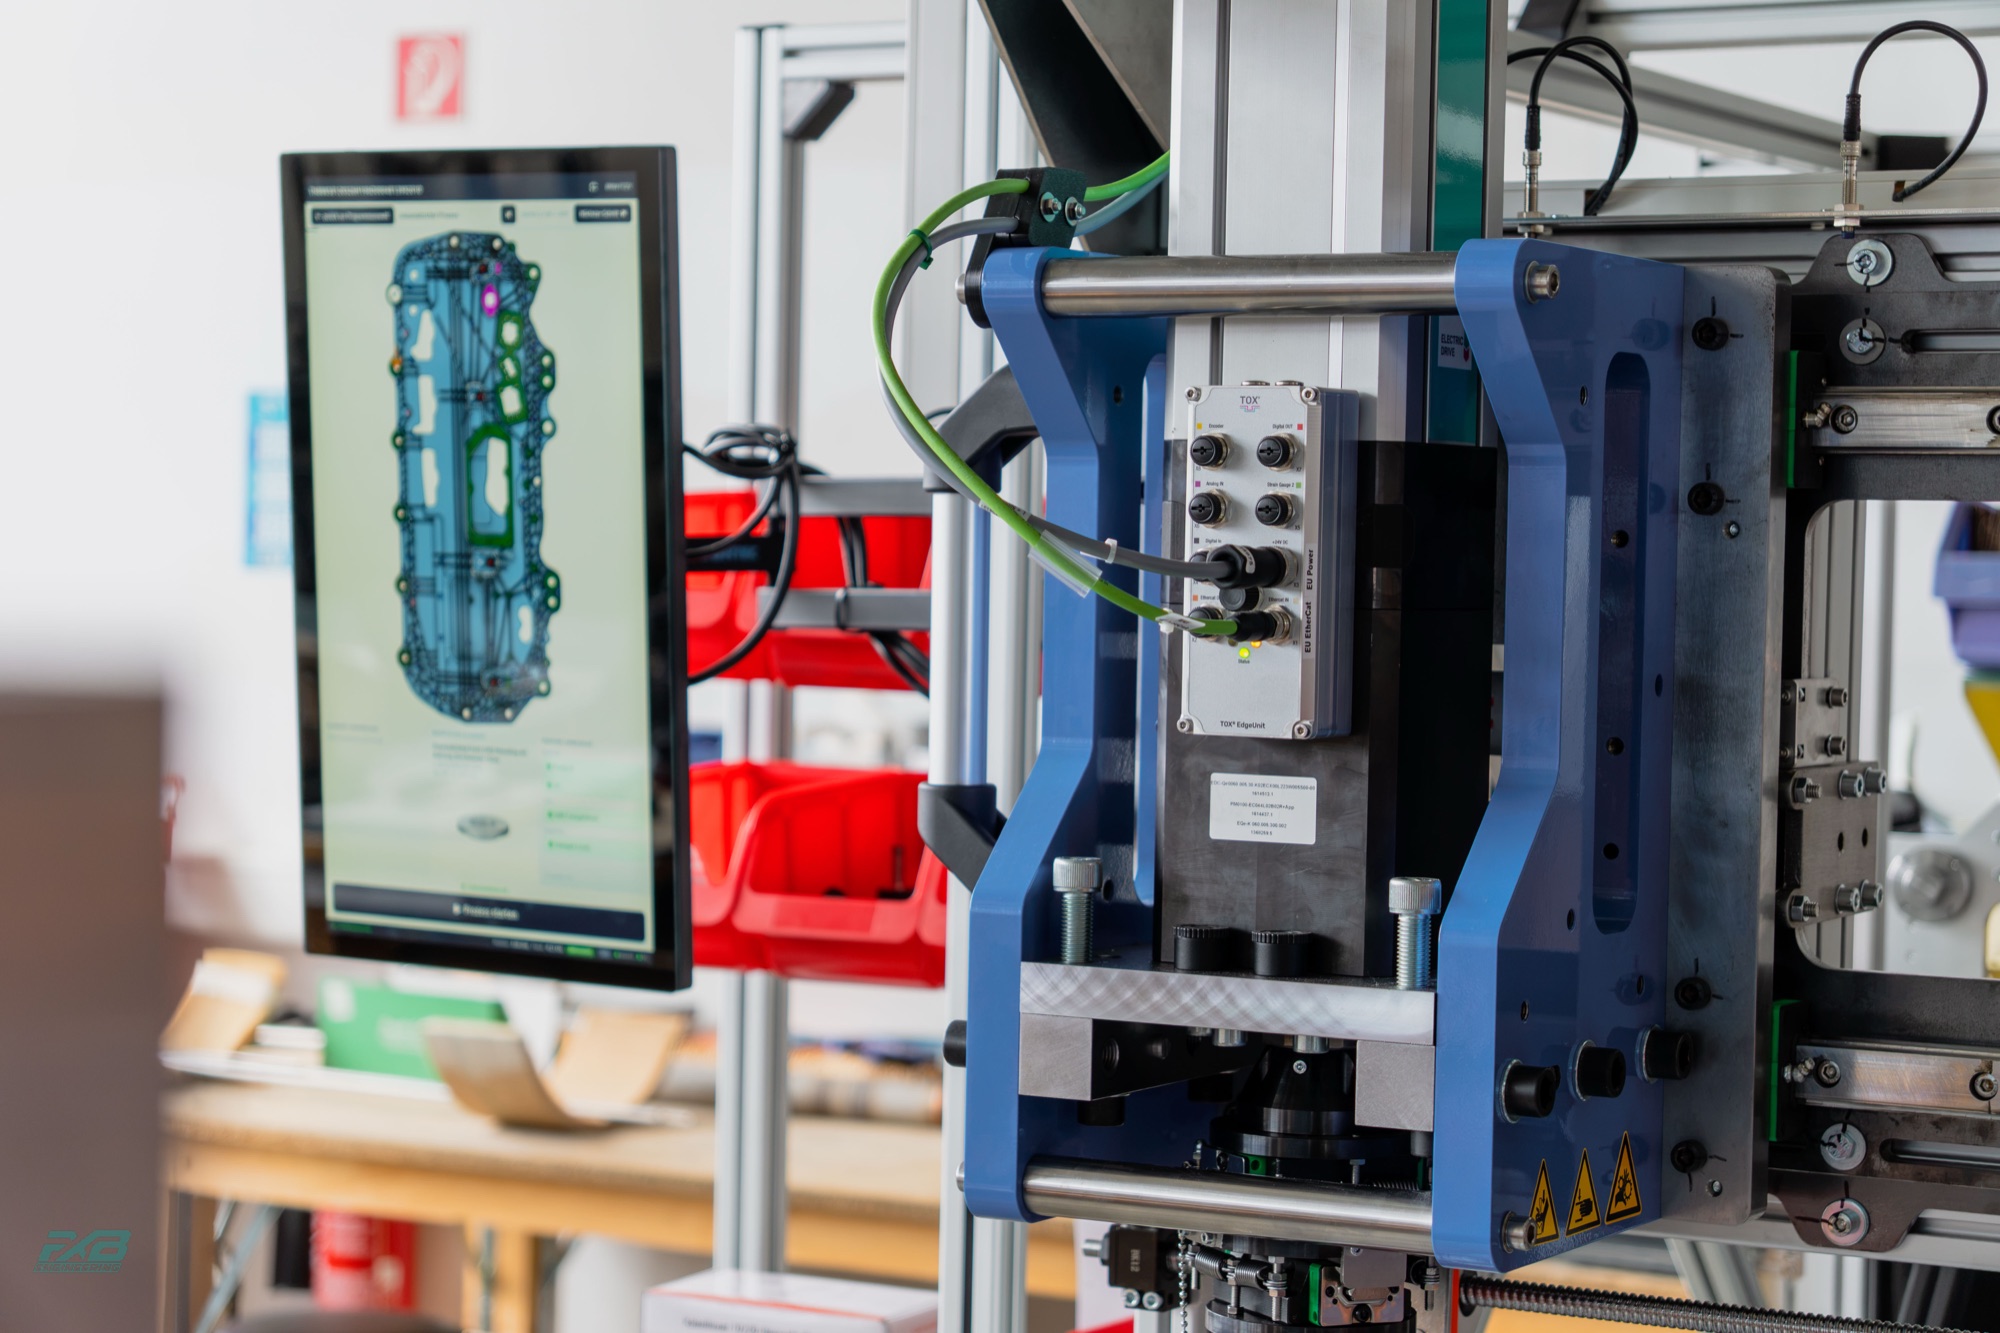
17 automatic press-in points with up to 60 kN press force and 13 manual screw-in positions at different X-Y-Z coordinates, with manual loading and unloading of the parts. Press forces must be logged per point, and the manual operations must be validated.
Solution
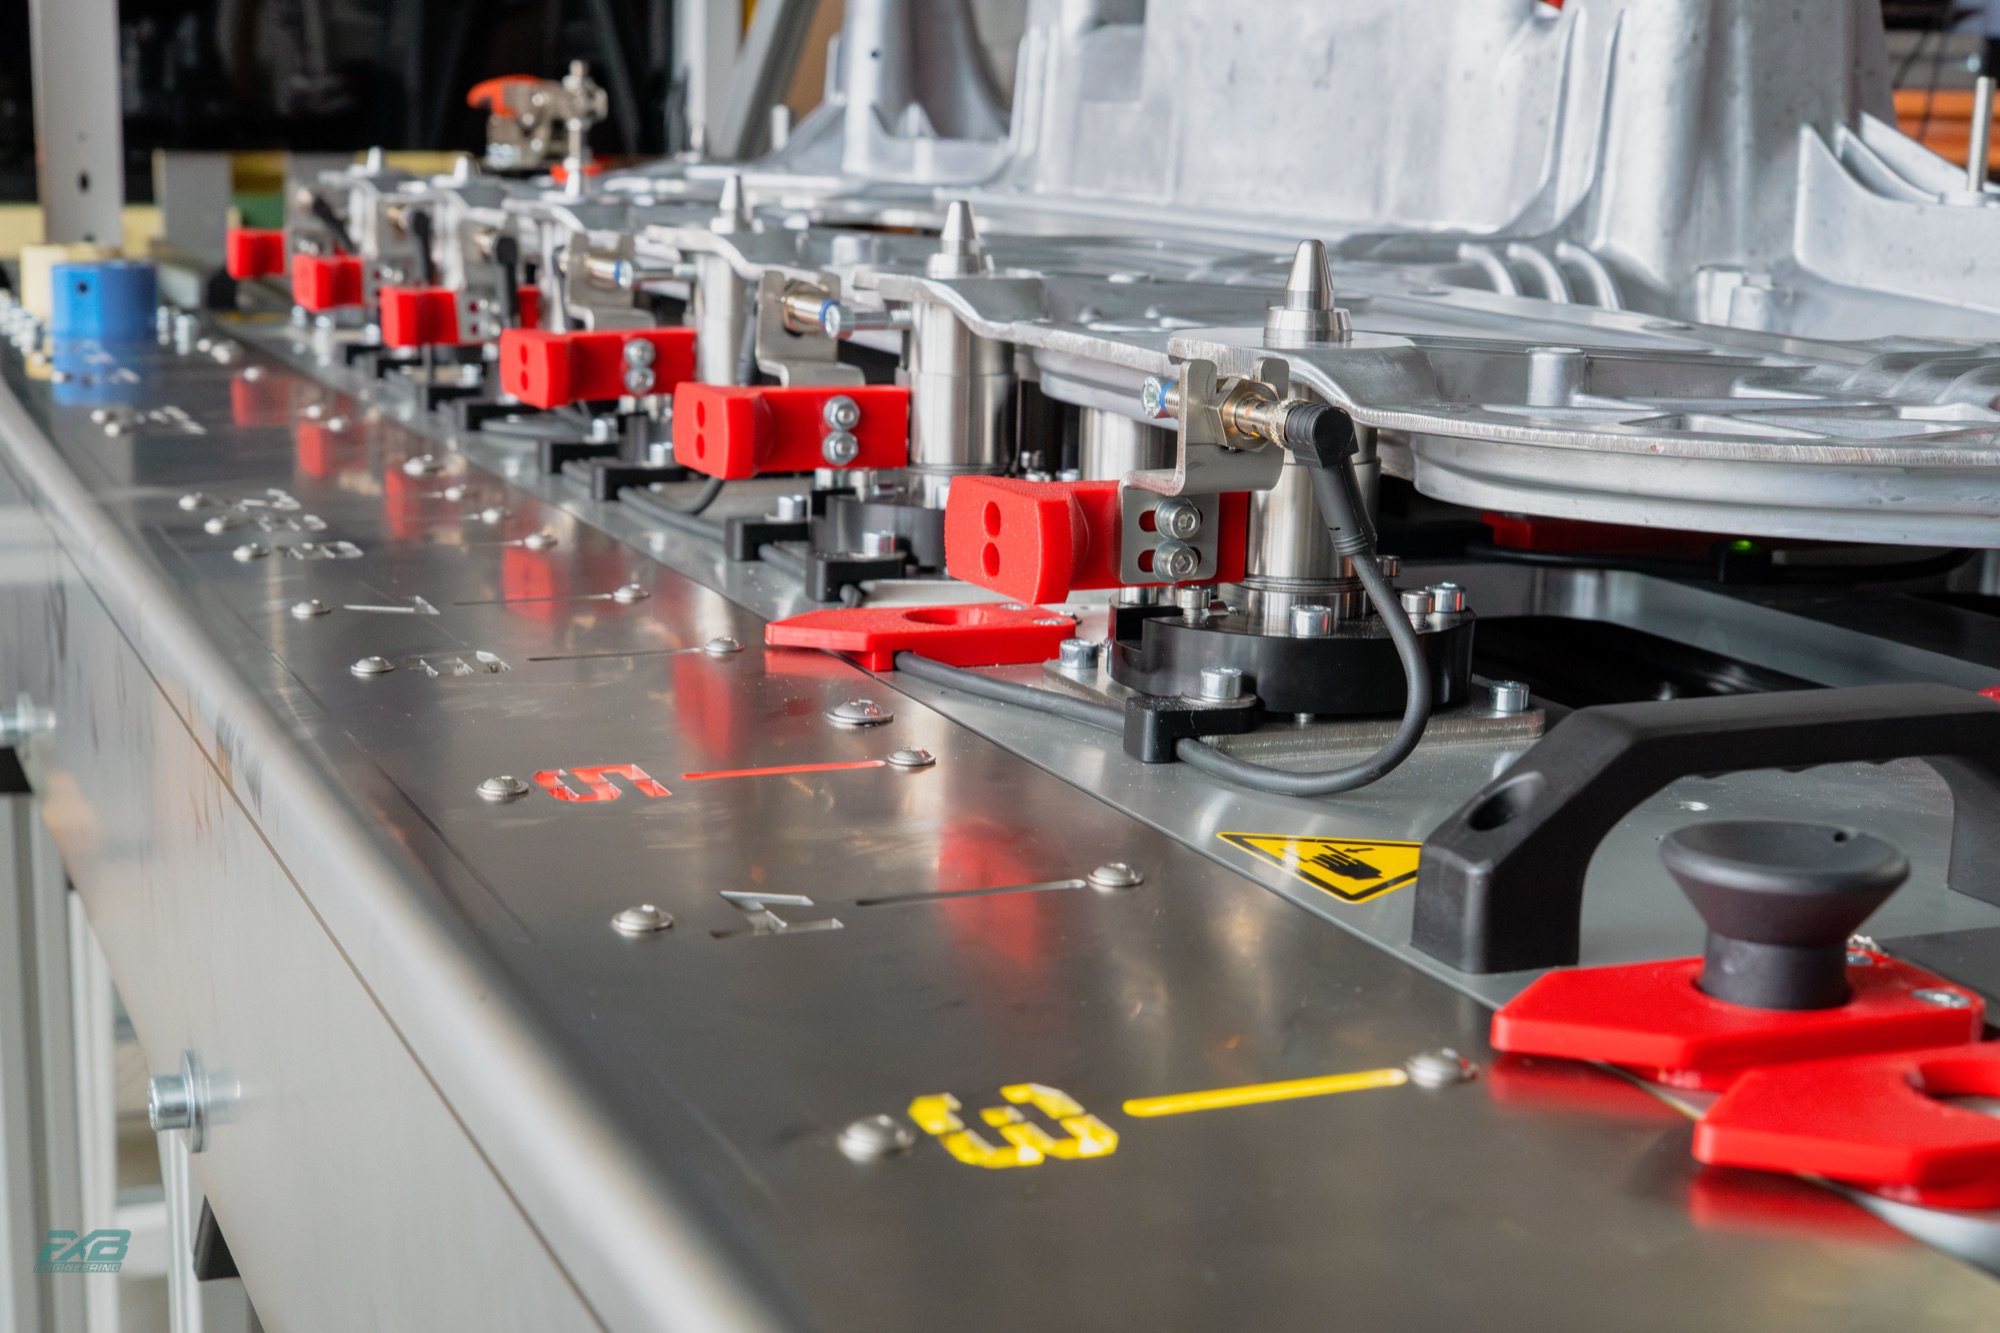
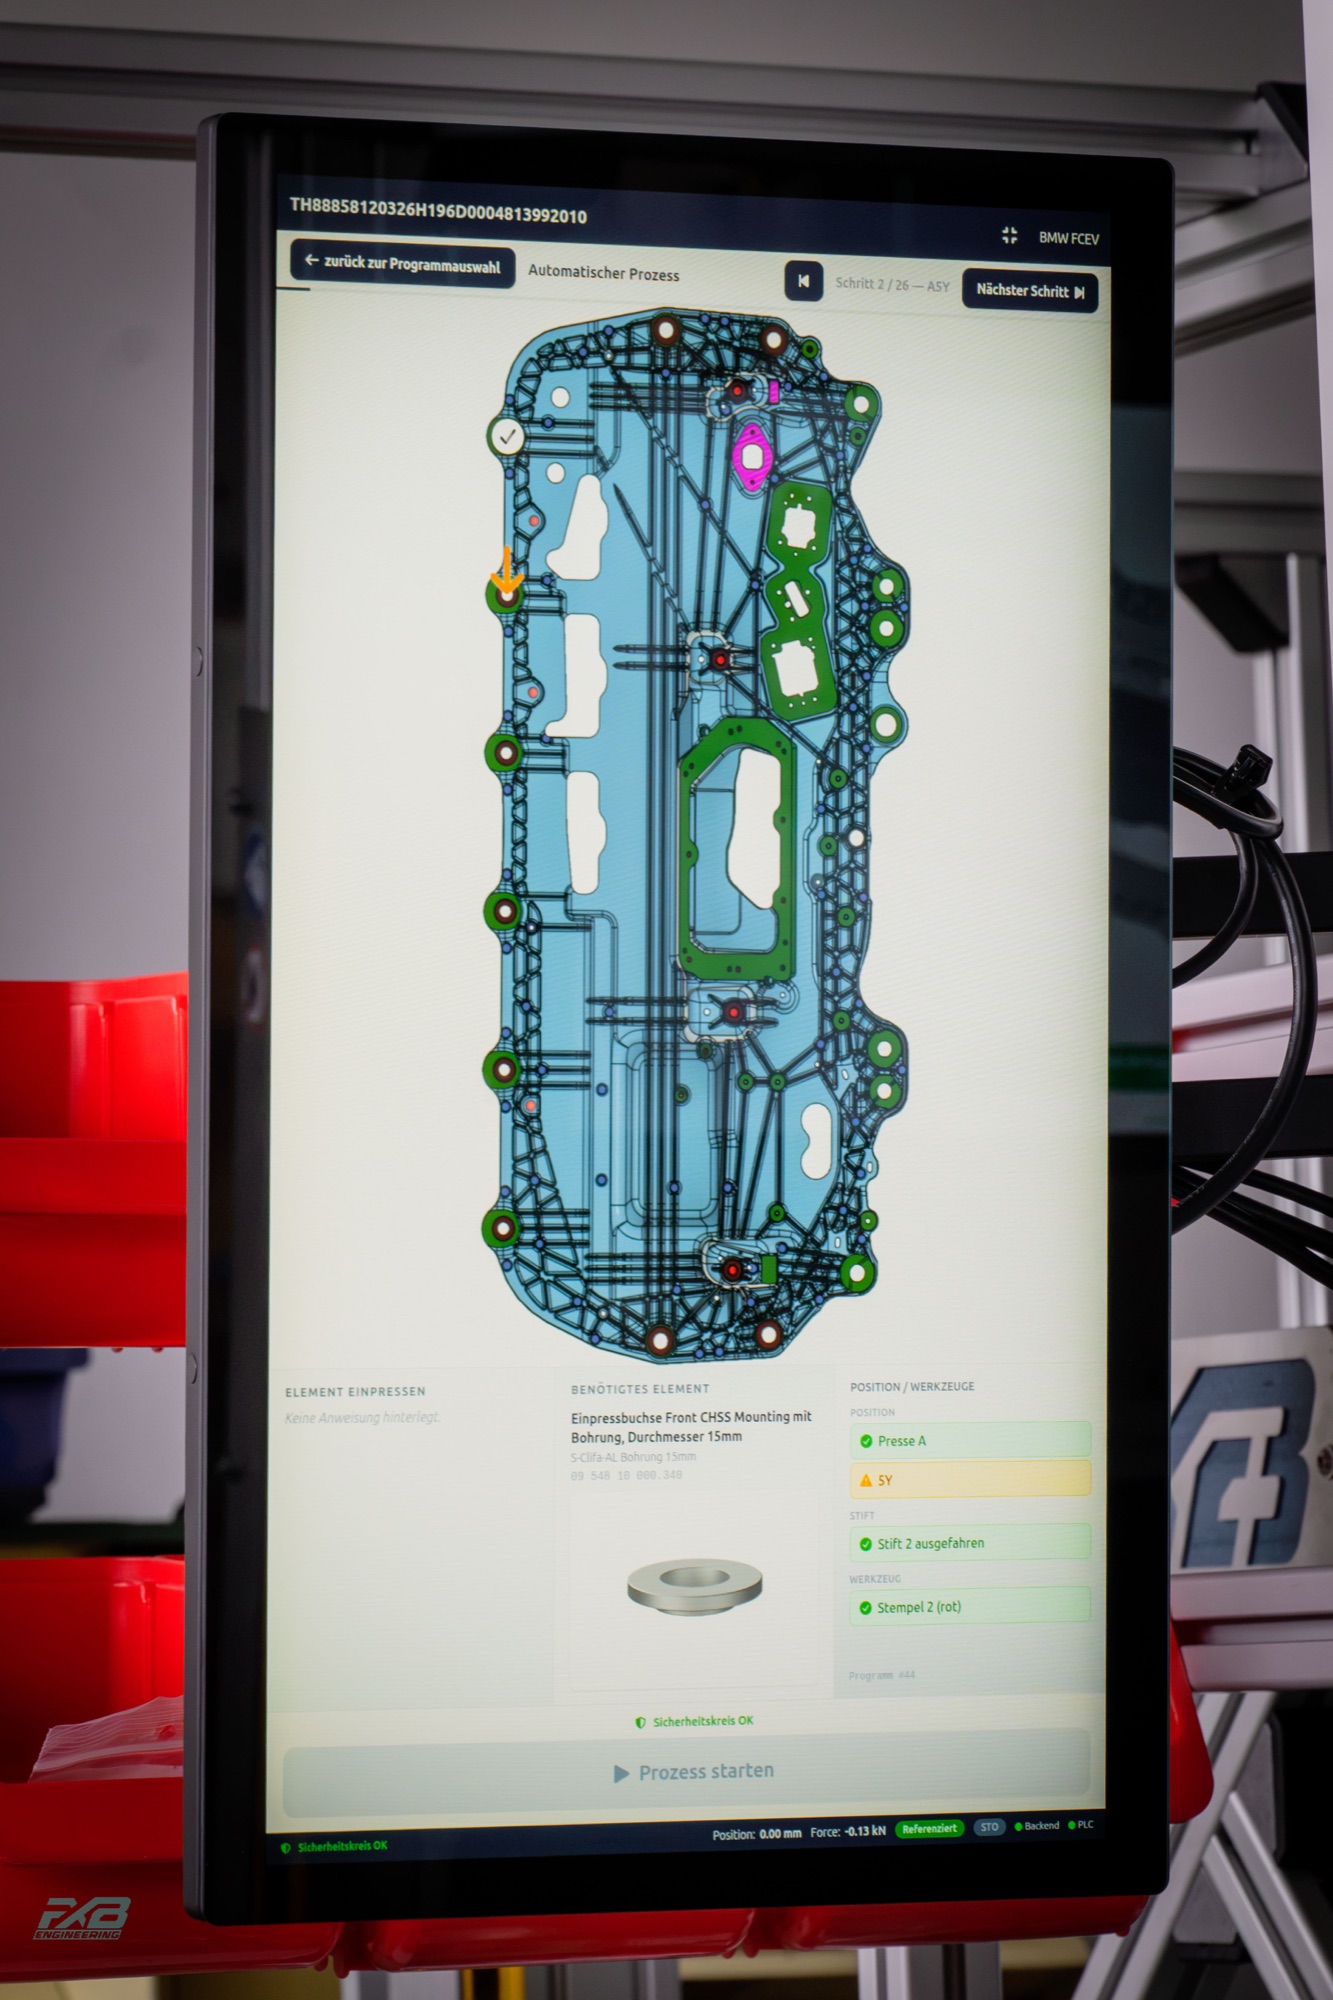
Planning, design, procurement, assembly, and commissioning of the assembly system. Parts and press unit are mounted on linear rails so that every joining position can be reached. Sensors confirm that each joining position has been reached, so a measurement report of the press forces is created at every joining point. Operators validate the manual screw-in positions with digital dial gauges; the results are transferred automatically to a database. Light curtains protect against the hazards of the system, and a custom HMI guides the operator through the process.
About this project
For NewAlu GmbH in Delbrück, FxB realized an assembly system that combines three work steps at a single station: pressing sleeves and threaded bolts into aluminium components, the manual assembly of special elements, and subsequent measurement. The scope covered planning, design, procurement, assembly, and commissioning. The system handles parts of up to 1250 x 530 x 180 mm.
Each component carries 17 automatic press-in points with up to 60 kN press force and 13 manual screw-in positions, spread across different X-Y-Z coordinates. Loading and unloading are manual. Every joint has to be proven correct: the press forces per point, the manual operations through validation.
Design
To reach every joining position, part fixture and press unit are mounted on linear rails. Sensors confirm that each joining position has been reached; on this basis, the system creates a measurement report of the press forces applied by the 60 kN joining spindle at every joining point.
The manual work steps are part of the same inspection chain:
- digital dial gauges validate the correct execution of the 13 manual screw-in positions
- all results are transferred automatically to a database
- light curtains guard the access area, with the safety functions running on a Beckhoff safety PLC
- a purpose-built HMI guides the operator step by step through pressing, assembly, and measurement
Result
Six months passed from planning to commissioning. The system was handed over with CE documentation and an operating manual. Every component leaves the station with a complete test report: documented press forces at 17 points and validated manual assembly at 13 positions. The mechanical design was carried out in Catia V6.